Tropical Climate Zone IVb Stability: Preventing Medical Packaging Failure in Humid Ports
How to prevent medical packaging delamination, carton collapse, and sterile barrier breach in humid tropical import ports under Climatic Zone IVb conditions.
Complete pre-shipment inspection (PSI) guide for medical consumables. Master ISO 2859-1 AQL sampling, sterile seal audits, and container loading checks.
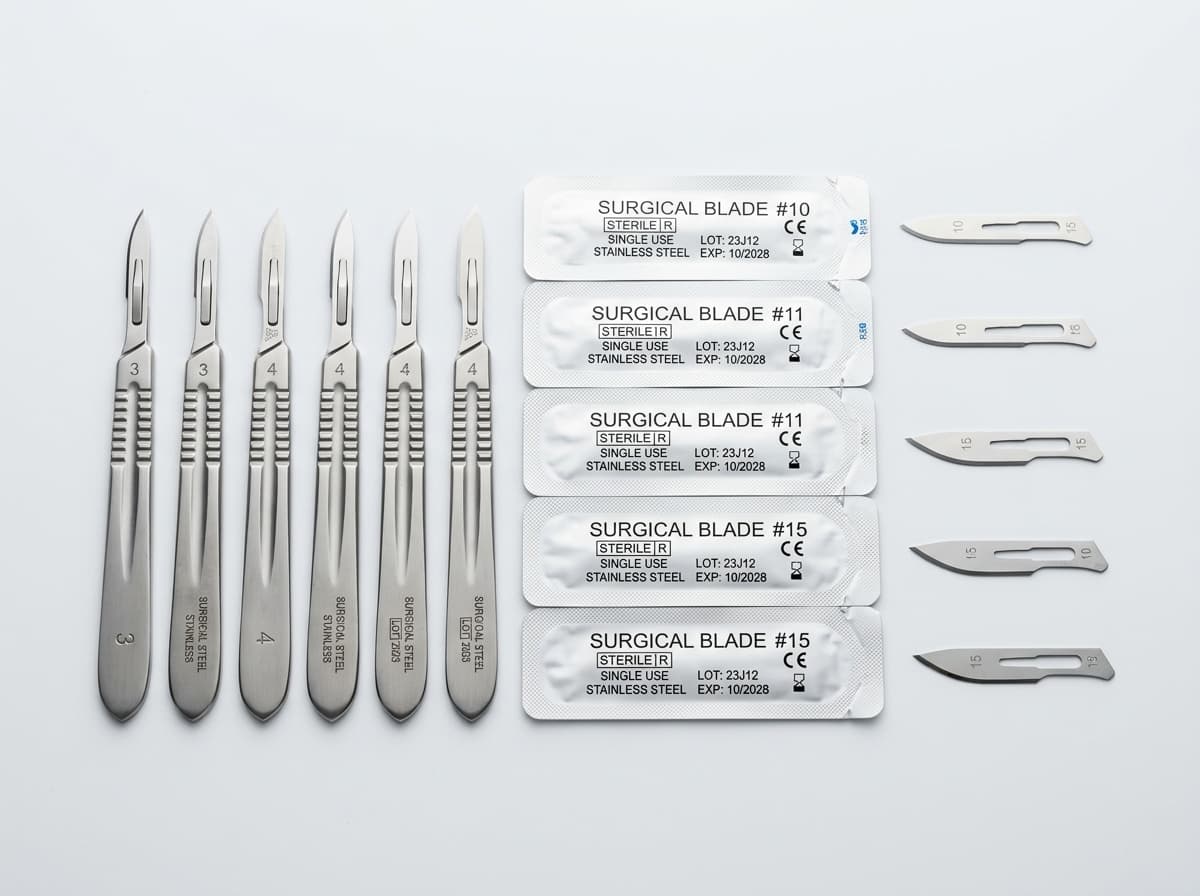
Complete pre-shipment inspection (PSI) guide for medical consumables. Master ISO 2859-1 AQL sampling, sterile seal audits, and container loading checks.
For sterile hospital consumables (such as surgical gloves, disposable syringes, and IV cannulas), international quality standards mandate an AQL 1.0 or AQL 1.5 Level II General Inspection Plan (conforming to ISO 2859-1 / ANSI/ASQ Z1.4). Inspection criteria divide into three defect tiers: - Critical Defects (AQL 0): Zero tolerance for compromised sterile packaging, mold, metal burrs, or foreign particles. - Major Defects (AQL 1.0 / 1.5): Functional issues such as loose hubs, sticky plunger movement, or illegible batch numbers. - Minor Defects (AQL 4.0): Cosmetic flaws such as slightly scuffed carton printing or minor label misalignment.
The table below outlines sampling sizes and acceptable defect thresholds for standard consumable import lots:
| Production Batch Lot Size | Sample Size Code Letter | Inspection Sample Size | Critical Defects (AQL 0) | Major Defects (AQL 1.5) | Minor Defects (AQL 4.0) |
|---|---|---|---|---|---|
| 3,201 to 10,000 pcs | Letter K | 125 units | Accept 0 / Reject 1 | Accept 5 / Reject 6 | Accept 10 / Reject 11 |
| 10,001 to 35,000 pcs | Letter L | 200 units | Accept 0 / Reject 1 | Accept 7 / Reject 8 | Accept 14 / Reject 15 |
| 35,001 to 150,000 pcs | Letter M | 315 units | Accept 0 / Reject 1 | Accept 10 / Reject 11 | Accept 21 / Reject 22 |
| 150,001 to 500,000 pcs | Letter N | 500 units | Accept 0 / Reject 1 | Accept 14 / Reject 15 | Accept 21 / Reject 22 |
If the number of defective units reaches the "Reject" threshold during sampling, the entire production lot is officially rejected. The manufacturer must quarantine the batch, re-inspect every carton, replace defective units, and bear the cost of a secondary inspection.
Beyond visual checks, a complete pre-shipment audit includes hands-on physical testing:
A production run can pass every bench inspection, only for goods to be ruined by poor container handling. The final stage of a thorough PSI is supervising container loading: 1. Container Weatherproofing Inspection: Inspect the empty ocean container from the inside with the doors closed. If you see pinpricks of daylight through the roof or door gaskets, the container will leak seawater during ocean transit. Reject the box and request a clean replacement. 2. Floor Dryness & Odor Check: The wooden floorboards of the container must be dry (moisture content < 15%) and free from industrial chemical smells, diesel oil residues, or mold. 3. Weight Distribution & Dunnage: Master cartons must be packed tightly without open voids. Airbags or dunnage bracing should fill gaps between pallets to prevent shifting in heavy seas. 4. Container Bolt Seal Verification: Once loading is complete, verify that the heavy-duty high-security bolt seal conforms to ISO 17712 (High Security Seal), and confirm that the unique seal number matches the bill of lading and export packing list.
When hiring third-party inspection agencies (such as SGS, Bureau Veritas, or Cotecna), issue an Inspection Work Instruction (IWI) that explicitly specifies functional tests. Generic inspectors often check only carton quantities and external labels while skipping critical dye-penetration and seal-strength tests.
Manshav Impex welcomes third-party pre-shipment inspections from SGS, BV, TUV, and client-appointed audit teams across our manufacturing and export packaging operations. Learn more about our quality control processes and cleanroom manufacturing facilities.
---
"Quality is not something you hope for when opening a container at destination; it is verified carton by carton before the container doors are closed."
---
Under standard international commercial trade practices, the buyer pays for the initial third-party inspection. However, sales contracts typically state that if a lot fails inspection, the manufacturer must cover the cost of all subsequent re-inspections after correcting the batch.
A **During-Production Inspection (DPI)** takes place when 20% to 40% of the run is completed, helping catch dimensional or packaging errors early. A **Pre-Shipment Inspection (PSI)** occurs once 100% of the goods are produced and at least 80% are packed into final shipping master cartons.
Visual seal inspection and laser scanning are non-destructive. However, dye-penetration testing (ASTM F1929) and tensile peel testing (EN 868-5) require opening and destroying sample packages. A small number of destructive test units is factored into standard quality sample planning.
The inspector issues a formal **Container Loading Supervision (CLS)** report containing photographs of the empty container, mid-loading progress, carton serial numbers, moisture desiccant placement, closed door latches, and the attached ISO 17712 security bolt seal.
Corrugated cardboard loses up to 50% of its vertical compression strength (BCT) when ambient humidity exceeds 80%. High-grade exporters use virgin kraft outer liners with moisture-resistant sizing to ensure lower carton layers do not crush during humid ocean transits. ---
How to prevent medical packaging delamination, carton collapse, and sterile barrier breach in humid tropical import ports under Climatic Zone IVb conditions.
Learn how private hospital networks optimize mixed-container medical consumable shipments from India. Reduce freight, manage MOQs, and streamline customs.
Guide to private-label medical consumables OEM sourcing in India. GS1 barcoding, UDI compliance, packaging artwork, and regulatory file creation.